Hookah Molasses Juice Separation, Aluminum Barrier & Cleanout Engineering
Technical specifications for handling 50–70% glycerin-molasses stickiness, preventing syrup phase separation, selecting 40–130 μm PET/Alu/PE barriers, and.
Contents in This Guide
Three Material Realities: Glycerin Migration, Volatile Terpenes & Sticky Cut Leaf
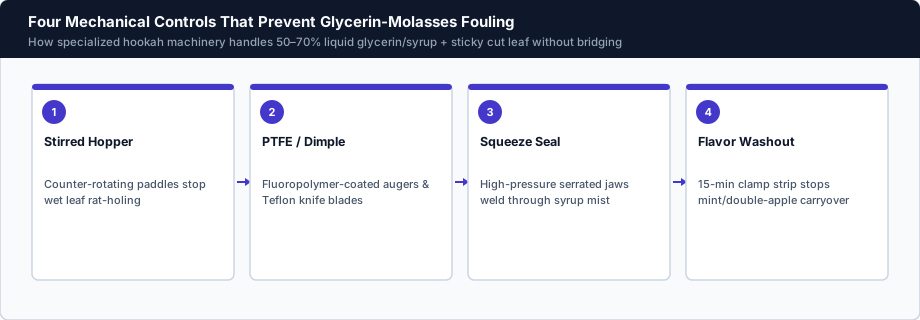
Well-rested shisha tobacco balances shredded leaf fiber, humectants (USP vegetable glycerin + propylene glycol), honey/molasses binder, and concentrated flavor esters (menthol crystals, trans-anethole in double apple, citrus terpenes). In packaging machinery, three failure modes appear immediately if specs are wrong: 1) Free syrup drains to the bottom of un-agitated hoppers, making early packs dry and late packs dripping wet; 2) Citrus and mint volatiles delaminate cheap adhesive-laminated films; and 3) Menthol/anise aromas Ghost into subsequent berry batches via porous silicone gaskets.
Specifying counter-stirred feed hoppers, extrusion- or solvent-free polyurethane PET/Alu/PE barrier foils, and PTFE/SUS304 quick-clamp wet paths eliminates all three.
Shisha Material & Packaging Engineering Standards
Published film, seal, and contact-surface specifications for maassel and herbal blends:
| Engineering Parameter | Recommended Specification | Defect Prevented |
|---|---|---|
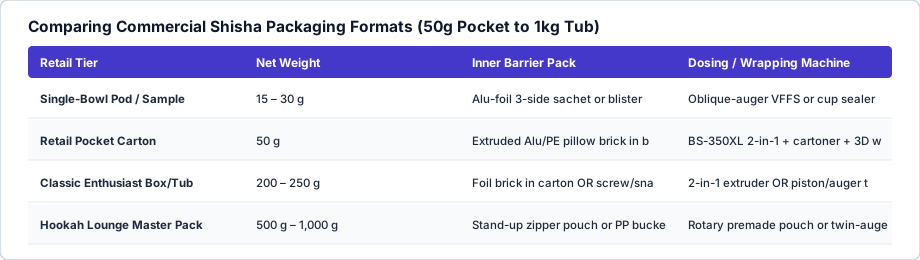
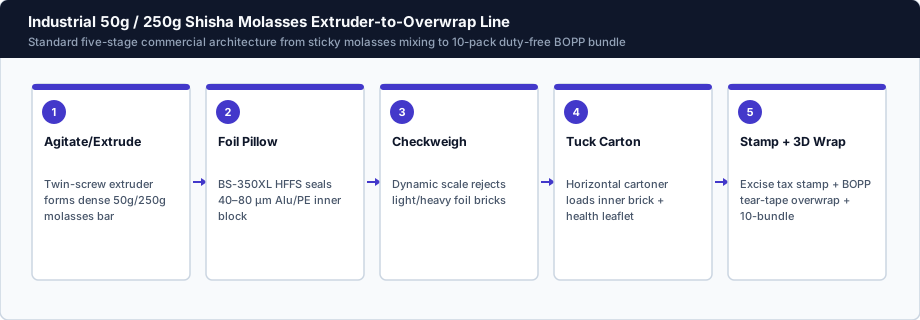
Inner Brick Foil (BS-350XL) |
40–80 μm OPP/VMPET/PE or PET/Alu7/LLDPE (<=350 mm web) |
Glycerin dry-out & aroma loss inside paper box |
| Stand-Up Zipper Pouch | 110–150 μm PET12 / Alu9 / PA15 / mLLDPE |
Citrus/mint delamination & oily zipper failure |
| Tub Induction / Heat Lid | PET/Alu35/PE peelable or weld foil liner |
Upside-down parcel syrup leaks in e-commerce |
| Contact Steel & Coating | SUS304/316L + PTFE/Teflon non-stick screw & rotary knife | Wet leaf balling on auger flights & blade drag |
| Elastomers & Gaskets | Virgin PTFE / FKM (avoid soft sponge silicone) | Anise / menthol flavor carryover between SKUs |
Estimate exact brick dimensions, film web widths, and hourly kg demand in our shisha line speed and kg/hr calculator.
Molasses & Barrier Engineering Notes
- mLLDPE / Ionomer Inner Sealants Weld Through Glycerin Mist: Glycerin boils near
290 °C—far above heat-sealing temperatures (135–165 °C)! Unlike water, glycerin droplets will not evaporate under a hot jaw; high-hot-tack metallocene LLDPE plus serrated high-pressure jaws physically squeeze syrup aside to fuse clean welds. - Dedicated Cheap Spare Auger/Funnel Sets for ‘Nuclear’ Flavors: Experienced hookah plants keep a second quick-swap stainless auger + nozzle tube (
~$900spare set) dedicated exclusively to Double Apple (anise) and Extreme Ice/Menthol to cut washdown downtime in half. - Ambient Room Temperature (
20–26 °C) Stabilizes Syrup Viscosity: Cold10 °Cwinter halls stiffen molasses into heavy putty, whereas35 °Csummer halls thin glycerin until free juice pools—climate-controlled packing rooms keep brick weights locked within±1–2%.
Compare Specifications Against Your Blend Profile
Share your glycerin/syrup %, leaf cut size (mm), and target pack weights via Project Brief or review sizing guides in shisha line sizing and buyer guides.
Compare related architectures in Shisha Packing Machines, Molasses & Barrier Specs, or submit your target pack weights via Project Brief.